Skip to content
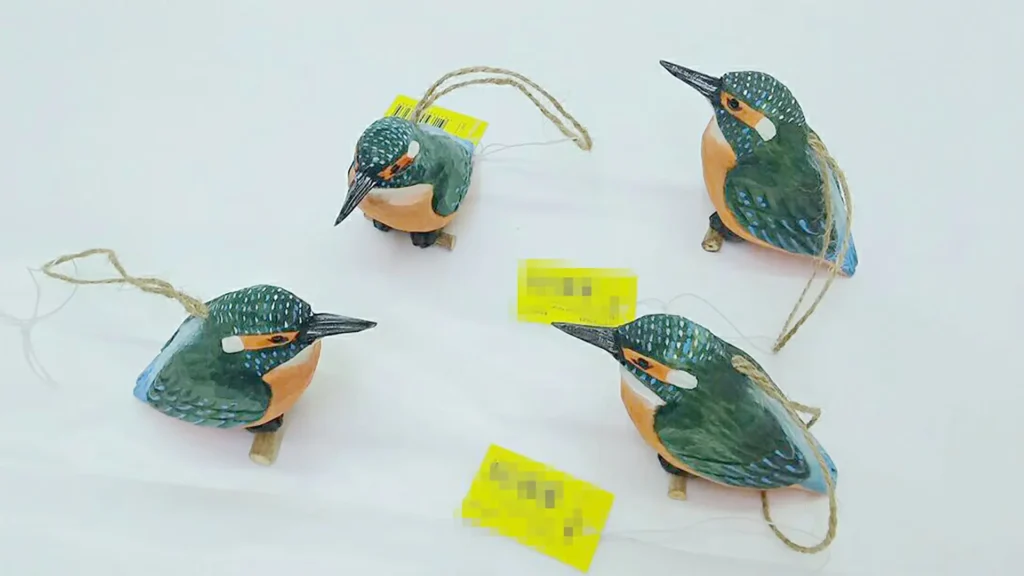
A final inspection tells you whether a shipment is acceptable, not why it failed — and by then the wood has been carved, painted and packed. Wooden ornament production is a sequence of decisions, and each leaves a mark no later stage can remove — so the checkpoints that protect your order sit inside the process, not at the end of it.
Below are the seven in-process checkpoints we run on every hand-carved ornament order, what each catches, and what to ask a factory to evidence. It is written for importers and private-label brands placing repeat orders. Still choosing a supplier? Start with our wood carving factory audit checklist.
Key Takeaways
- Seven checkpoints carry an order: timber identity, moisture, carved geometry, assembly and edges, finish and colour, safety documentation, packing. Each catches a defect class the next stage cannot repair.
- Moisture is the most-skipped check and has the longest tail. Wood held at 8–12% before finishing moves far less in a heated stockroom.
- Colour is judged against a physical golden sample, never a screen.
- A piece rejected at sanding costs a blank. Rejected after four coats of paint, it costs the labour, the drying space and the delivery window too.
- AQL tells you what to accept from a finished lot; in-process checkpoints reduce how many defects enter it. They are not substitutes.
- Ask for evidence, not adjectives: a moisture reading, a drop-test record, coating reports, and photos and video before balance payment.
In This Guide
- Why In-Process Checks Beat a Final Inspection
- Checkpoints 1 and 2: Timber Identity and Moisture
- Checkpoints 3 and 4: Geometry, Assembly and Edges
- Checkpoints 5 and 6: Finish, Colour and Safety Documents
- Checkpoint 7: Packing and the Drop Test
- The Seven Checkpoints in Wooden Ornament Production
- Best For / Not For: Inspection Depth by Buyer Type
- What We Check Before an Order Ships
- End to End: A First Custom Ornament Run
- Frequently Asked Questions
Why In-Process Checks Beat a Final Inspection
Hand-carved pieces are made in stages that each destroy the evidence of the last. Once a piece is painted you cannot see the tear-out underneath. One inspection at the end of that chain samples six unchecked decisions and returns a single number.
There is also a consistency argument specific to handwork. No two carved pieces are identical, and that variance is part of what a customer pays for. Variance inside an accepted range is craft; outside it is a defect. Holding that line across thousands of pieces means checking against a retained physical reference at every stage, not once at the end.
Checkpoints 1 and 2: Timber Identity and Moisture
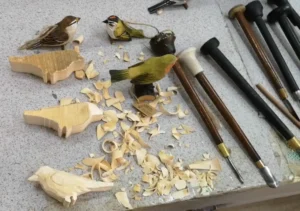
1 — species and grade at intake. Before anything is cut, timber is verified against the specification: species, grade, dimension. We carve in basswood, pinewood, rubber wood and birch, and each behaves differently under the knife and under paint. Basswood holds fine detail because it is pale and fine-grained; pine carries figure that reads rustic and can telegraph through a light paint. A substitution at intake is invisible at the end of the line, which is why it is checked first. Grade matters equally — knots, resin pockets and end-splitting become a rejection after four hours of work if they are not screened out at the start.
2 — moisture before machining. Wood is held between 8% and 12% before finishing, per our published wood moisture content standard. This check has the longest failure tail: wood that ships wet keeps moving for months, cupping, splitting along the grain and cracking the paint film from underneath. The buyer sees it in February on a shelf and cannot trace it to a drying rack in October. Destination sets the target — a dry continental winter interior asks something different of the wood than a humid coastal market.

Checkpoints 3 and 4: Geometry, Assembly and Edges
3 — size and weight after carving. Pieces are measured against the drawing, and three dimensions matter commercially. An ornament 4 mm deeper than specified will not close its gift box. Retail fixtures are planned by depth, and a run that drifts will not sit on the peg the buyer already committed to. Weight drives freight: a master carton packed at the top of its tolerance is a different landed cost per piece than one at the bottom. Our range runs from 5 cm miniatures to 40 cm three-dimensional pieces, with flat carving to 80 cm — and a tolerance invisible on a 5 cm bird is obvious on a 40 cm one, so tolerance is set per size band.
4 — assembly, hanging hardware and edges. This is what customers feel before they see. Hanging holes tear out if the drill exits too fast, and cord attachments are a safety matter as well as a cosmetic one: an ornament that drops off a tree is a returned ornament. Sanding burrs and the crispness of edges later outlined in paint are judged here. Multi-part pieces are checked for joint integrity before paint hides the seam, because glue starvation shows as a hairline afterwards and cannot be fixed without stripping.

Checkpoints 5 and 6: Finish, Colour and Safety Documents
5 — colour and detail against the retained sample. Every piece is carved and painted by hand, so colour is judged against a physical approved sample under consistent light, not a photograph or a monitor. Checking here rather than at packing means a drift in a paint mix is caught on the twentieth piece, not the two-thousandth. Match and coverage are judged together: paint laid too thin over pale basswood looks different under retail LED than in the workshop, and a wandering detail line is far more visible to a shopper than to the person painting the fiftieth piece of the morning.
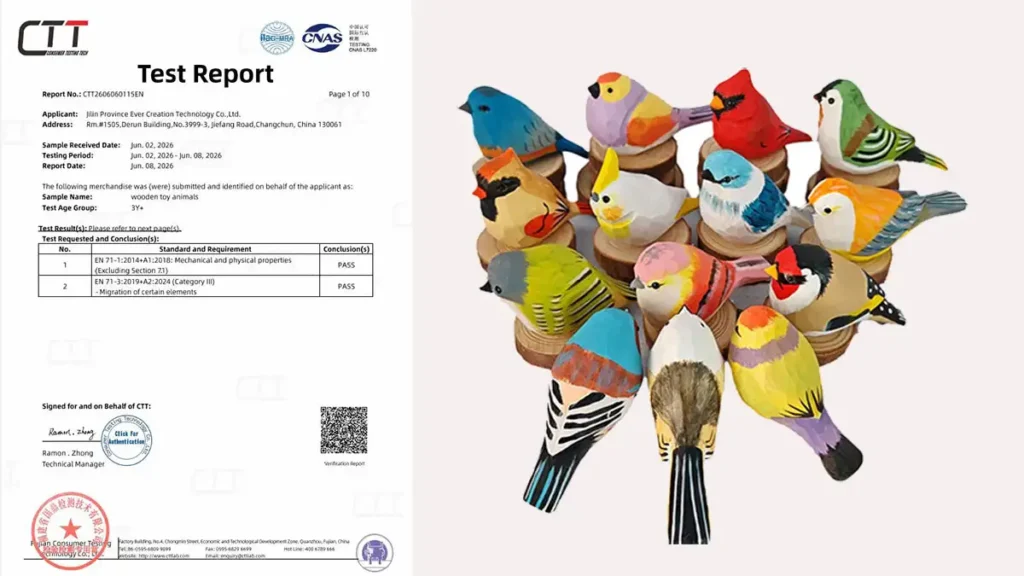
6 — safety documentation and labelling. Where an ornament could reasonably end up in a child’s hands, the finish is regulated: coatings must meet the migration limits of the EN71 toy safety standards and small-parts sizing applies. Even where a piece sells as decoration, age-warning labelling must suit the market it enters: an ornament that looks like a toy is treated as one by customs. The output here is a document, not a judgement. Our facility operates under ISO 9001 and BSCI, with CE, RoHS and UKCA protocols on electrical lines; the EN71 route is the relevant one for painted articles children may handle, detailed in our guide to EN71 compliance for wooden products.
Checkpoint 7: Packing and the Drop Test
The last checkpoint survives the longest stretch of handling. Each piece is wrapped in white paper, 6 to 12 go into a three-ply inner box at 21 × 11 × 14 cm, and 240 to 480 into a five-ply master carton at 58 × 44 × 31 cm, gross weight held at 8.0 to 15.0 kg. Cartons are rated to pass an ISTA 3A drop test, simulating a real distribution chain rather than a gentle warehouse.
Three easily missed points: the pack pattern must match the carton count the buyer’s system expects, since a retailer planning on 240 per carton who receives 480 has a stockroom problem, not a quality one; inner boxes must be filled rather than rattling, because movement inside a box is abrasion and abrasion shows as a rub mark on paint; and hang tags and shipping marks must carry approved artwork. See our guide to B2B export packaging for handcrafted wood carvings.

The Seven Checkpoints in Wooden Ornament Production
An acceptance sampling plan such as AQL answers one narrow question — given a finished lot, how many pieces do I inspect and how many defects make me reject it. It does not reduce the defects inside that lot, which is what the checkpoints below do. A factory that can quote a level but cannot describe what happens between intake and packing is offering the certificate and not the process. See our guides to AQL inspection levels for wooden crafts and pre-shipment QC for wholesale ornaments.
| Checkpoint | Catches | If skipped, surfaces as |
|---|---|---|
| 1. Timber identity and grade | Wrong species, knots, resin pockets, end-splitting | Detail that will not hold; grain showing through paint |
| 2. Moisture content | Wood outside 8–12% before finishing | Cupping, splits and cracking months later, in store |
| 3. Size and weight | Dimensional drift from the drawing | Boxes that will not close; fixtures that will not hold |
| 4. Assembly and edges | Torn hanging holes, weak joints, burrs | Ornaments dropping off trees; seams opening later |
| 5. Colour and detail | Drift from the approved golden sample | A run that does not match itself on the shelf |
| 6. Safety documentation | Missing coating reports, wrong age labelling | Held at customs; rejected by a compliance team |
| 7. Packing and drop test | Wrong pack pattern, loose inners, unverified cartons | Breakage and rub marks on arrival |
Best For / Not For: Inspection Depth by Buyer Type
| Buyer type | Strong fit | Wrong emphasis |
|---|---|---|
| Private label, repeat designs | Checkpoints 1, 2, 5 — a retained sample plus a stated moisture range keeps run twelve looking like run two | Heavy first-article inspection on every reorder once the spec is frozen |
| Seasonal importer, one annual buy | Checkpoints 3, 6, 7 — dimensions that fit fixtures, documents that clear customs, packing that survives peak freight | Treating the golden sample as optional; there is no run history to lean on |
| Gift retailer, in-stock designs | Checkpoint 7 and a standard sampling plan — the design is proven, so your risk is transit and pack count | Full in-process oversight on a 100-piece trial, which costs more than the risk it retires |
| Chain or marketplace seller | Checkpoint 6 above all — labelling, small parts and coating documents are audited first | Assuming a boutique’s aesthetic tolerance; a chain’s is tighter and must be written down |
What We Check Before an Order Ships
- Species and grade at intake, against the order specification, with boards carrying knots or end-splitting pulled before machining rather than after painting.
- Moisture held at 8–12% before finishing, targeted against the destination climate.
- Carved geometry measured against the drawing, tolerance set per size band across our 5 cm to 40 cm range and to 80 cm for flat carving.
- Colour judged against the retained golden sample under consistent light, early enough that drift is caught in tens of pieces rather than thousands.
- Finish documentation and labelling confirmed for the destination market, including EN71 coating reports where a child may handle the piece.
- Pack pattern, carton count and drop-test rating confirmed — white paper wrap, 6–12 per three-ply inner box, 240–480 per five-ply master carton, 8.0–15.0 kg gross, rated to ISTA 3A.
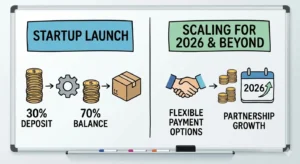
- Photos and video of finished goods sent before balance payment, under our T/T terms of 30% deposit and 70% before shipment.
One honesty note on materials. Our facility holds FSC chain-of-custody certification and operates under ISO 9001 and BSCI, but certified basswood is not currently available to us, so we do not market our carvings as made from FSC-certified wood; we can supply official timber felling and transport permits instead. Raise certified-material requirements before sampling — see our guide to ESG and sustainable sourcing for wooden decor.
End to End: A First Custom Ornament Run
A European gift wholesaler wants a custom hand-painted range for the following Christmas, sold into independent shops and one regional chain.
Sample. Designs arrive as multi-angle references with a target size and species. A trial order of 100 pieces at a USD 500 minimum order value goes air express on DDP terms and lands in 20–30 days. Those pieces get hung, dropped and photographed in a shop window; the approved one becomes the golden sample retained by both sides.
Specification freeze. Species, tolerance per size band, sanding finish, hanging hardware, paint system, packaging tier and labelling artwork are written down, so checkpoints 1 to 6 have something to check against. That handover is sequenced in our guide to the wood OEM timeline from sample to first order.
Production. The order moves to the wholesale tier at 300 pieces and a USD 3,000 minimum order value, sea freight, 60–90 days to port. Timber is verified and moisture-checked at intake, geometry measured after carving, colour judged against the retained sample through the painting run.
Documentation and packing. EN71 coating reports are matched to the paint actually used and age labelling checked against destination rules — the chain asks for these before listing, not after arrival. Custom printed boxes go in at the 500-piece minimum and cartons are drop-tested.
If something still goes wrong. A small share of a hand-made run is always arguable. What matters is that a documented reference exists on both sides, which turns a dispute into a comparison — see quality claims and defect resolution.

If you want to see how these checkpoints apply to your own design and volume — including the sample stage, carton quantities and the documentation your channel requires — send us your references and we will build the specification with you.
Frequently Asked Questions
Q: How many quality checkpoints should a wooden ornament order have?
Seven cover the process end to end: timber identity and grade, moisture, carved size and weight, assembly and edges, colour against the approved sample, safety documentation, and packing with a drop test. Fewer leaves a stage where a defect can be created and then concealed by the next one.
Q: What moisture content should wood be at before finishing?
We hold wood between 8% and 12%. That range limits the movement causing cupping, splitting and paint cracking once a piece reaches a different climate. Where in the range you aim depends on the destination market.
Q: Is an AQL inspection enough on its own?
No. Sampling decides whether to accept a finished lot; it does not reduce the defects inside it. In-process checkpoints do that, and the sampling plan then verifies the result.
Q: What evidence should I ask a factory to provide?
A moisture reading, the retained golden sample reference, coating test reports where a child may handle the piece, a drop-test record for the carton specification, and photos and video of finished goods before balance payment.
Q: Can hand-carved pieces be consistent enough for a chain retailer?
Yes, if consistency is defined rather than assumed. State the dimension tolerance per size band, judge colour against a physical sample, and document the acceptance rule. Written that way a hand-carved run is auditable in the same terms as a machine-made one.
Sources
EN71 migration limits for coatings on articles children may handle are published by the European Commission; United States importers can work through the route map at the Consumer Product Safety Commission. Our moisture range, size range, species list, carton specifications and ISTA 3A rating, minimums, lead times and payment terms are our own published first-party terms. No defect-rate or acceptance-percentage figure is quoted, because those are set per order.